
ABS is the material you reach for when a printed part has to survive handling, heat and chemicals, and it is also the material that punishes a printer with a sloppy thermal environment. We spent weeks with ten enclosed machines to work out which ones actually hold their chamber steady while an ABS part is cooling. Here is the short version: the Creality K2 Pro Combo is the one we would buy, because its actively heated 60°C chamber and 350°C steel-tipped nozzle mean tougher engineering blends need no hardware upgrade later.
If you want a second opinion before you commit, our broader guide to the best 3D printers covers the machines that do not need an enclosure at all, and our filament buying guide covers the material side of the equation.
That is the whole problem with ABS in one paragraph. The plastic has a glass transition temperature near 100°C and it shrinks roughly 1% as it cools, so if the bottom of a part solidifies faster than the top, internal stress builds and the corners lift off the bed. An enclosure blocks drafts and traps heat. An actively heated chamber goes further and holds the air above 40°C for the entire print.
That is why we sorted these ten machines on chamber temperature first and everything else second. Speed ratings, AI cameras and multi-colour units are nice, but they do not stop a part from cracking along its layer lines.
Table of Contents
Top 3 Picks for ABS Printing in 2026


All three of those machines run a fully enclosed chamber with real filtration, and all three reach at least a 280°C nozzle, which is the practical floor for ABS and anything you blend into it. The difference between them is how much heat the chamber holds and how much extra hardware you carry for multi-material work.
Best Enclosed 3D Printers for ABS Printing (October 2026)
| Product | Specifications | Action |
|---|---|---|
 Creality K2 Pro Combo |
|
Check Latest Price |
| Flashforge Creator 5 Pro Multi-Color |
|
Check Latest Price |
| Flashforge Adventurer 5M Pro |
|
Check Latest Price |
 QIDI Plus4 |
|
Check Latest Price |
 Flashforge Creator 5 Pro Enclosed |
|
Check Latest Price |
 Creality K2 Plus Combo |
|
Check Latest Price |
 Creality K1C |
|
Check Latest Price |
 Bambu Lab P1S Combo |
|
Check Latest Price |
 ELEGOO Centauri Carbon 2 Combo |
|
Check Latest Price |
 Creality K2 Combo |
|
Check Latest Price |
A note on reading that table: the chamber column is the one that separates a reliable ABS machine from a hopeful one. Five of the listings here hold an actively heated chamber, and the rest depend on the enclosure alone.
1. Creality K2 Pro Combo – Best Overall for ABS
Official Creality K2 Pro Combo 3D Printer Multicolor Printing with CFS
Active chamber 60C
Steel nozzle 350C
40mm3/s hotend
CFS 16 colours
Pros
- Active 60C chamber cuts corner warp on ABS ASA and PPA
- Steel-tipped nozzle rated to 350C for abrasive filaments
- 40mm3/s hotend sustains strong ABS flow at 280C
- Dual AI cameras catch flow faults and print failures
- Hardened steel gears and a modular quick-swap hotend
Cons
- Seller support quality varies between listings
- 23 x 23 x 24 inch frame and 52 pounds need a solid bench
- CFS multicolor adds purge tower time and filament waste
This is the machine our team keeps coming back to. The chamber is actively heated to 60°C rather than simply enclosed, which means a tall ABS enclosure prints with the same thermal conditions at layer 20 and layer 400. The steel-tipped nozzle is rated to 350°C, so when you move from plain ABS to PC-ABS or a carbon-fibre reinforced blend later, the hotend is already there.
The 40mm³/s high-flow hotend with an 80W heater is the other half of the story. ABS flows badly when it is cool, and a marginal hotend shows up first as under-extrusion at the infill. This one is specified to push 40mm³/s of ABS at 280°C, which is where the fast 600mm/s motion actually becomes usable rather than decorative.
Two AI cameras do real work here rather than sitting there for time-lapses. The nozzle camera adjusts flow in real time, and the chamber camera catches spaghetti failures, foreign objects and a nozzle that has stopped extruding mid-print. For long ABS jobs, that is the difference between a lost night and a morning coffee.
Smart auto levelling probes only the area of the bed the model will occupy, which saves time on small parts and avoids probing zones you will not print on. Hardened steel drive gears matter more than they sound once you start running abrasive filament through the same extruder.
What the actively heated chamber actually changes
Passive enclosures hold drafts out and stop airflow across the part. Active heating does something different: it raises the temperature of the air the part is cooling into, so the layer below stays above its softening point longer while the new layer is laid down. Corner lift depends on that temperature difference, and removing it removes most of the problem.
The practical difference shows up on large flat parts and tall thin walls, which are exactly the shapes that warp first. On a smaller part printed in a couple of hours, the K2 Pro’s chamber handling is a margin of safety rather than a rescue.
Where you feel the trade-off
This is a 52-pound machine in a 23 x 23 x 24 inch frame. It needs a bench that is level and can carry it, and a clearance above the door for extra CFS boxes if you expand beyond the single one. In a small home office that is a real constraint.
The multi-colour CFS adds a purge tower to every colour change, which is time and waste you do not need for single-colour ABS work. If ABS is the only reason you are buying, you are paying for capability you will not use.
2. Flashforge Creator 5 Pro Multi-Color – Best Value All-Rounder
FLASHFORGE Creator 5 Pro Multi-Color 3D Printer,4-Toolheads,Fully Enclosed
Active chamber 65C
HEPA 13 plus carbon
Bed 120C
4 toolheads
Pros
- Four toolheads give true multi-material prints with no purge waste
- 65C active chamber is the strongest warp defense in this group
- HEPA 13 and activated carbon capture dust and VOCs
- Dynamic flow compensation calibrates all four nozzles
- Quiet at 55dB or less for overnight runs
Cons
- Four toolheads add mechanical complexity
- More wear points and possible calibration drift over time
The chamber here is actively heated to 65°C, the joint-highest figure in this roundup, and the bed reaches 120°C. For ABS that combination means the bed is well above the glass transition temperature of the plastic while the part is bonding to it, so first-layer adhesion stops being a daily argument.
What makes this machine different is the four-toolhead arrangement. Each hotend has a dedicated nozzle for one material, so switching colours and materials takes seconds and there is no purge tower. Printing a shell in one colour with a stiff infill in another is genuinely useful on functional ABS parts.
Filtration is a real consideration rather than a checkbox here. The built-in HEPA 13 filter handles particles and the activated carbon layer handles the styrene vapour that gives ABS its smell, and the whole system runs at 55dB or below. That combination is what makes an ABS machine reasonable in a home or a shared studio.
Calibration is fully automatic with dynamic flow compensation across all four nozzles, and the CoreXY frame travels at 600mm/s with up to 30000mm/s² acceleration. We would leave ABS volumetric speeds conservative regardless, but the frame is stiff enough that you can push when the geometry allows it.
What four independent toolheads buy you
On a normal single-extruder machine, a colour change means heating the nozzle up, pushing material through, and wiping it out. On a four-toolhead machine the machine simply swaps heads. For an ABS job with a TPU seal or a contrasting marker layer, that saves a large amount of time and filament.
It also means each material keeps its own nozzle, so abrasive filament does not chew the nozzle you use for clean ABS detail work. On machines that share one hotend, that wear is shared too.
What four independent toolheads cost you
Every hotend is a heater block, a thermistor, a nozzle and an extruder that can all need attention. Four of them is four times the maintenance surface, and a machine that has been running for two years may need recalibration across all four.
If you only ever print one material, all of that hardware sits idle. A single-extruder machine with a simpler build would serve you better.
3. Flashforge Adventurer 5M Pro – Budget Pick
FLASHFORGE Adventurer 5M Pro 3D Printer with 1 Click Auto Printing System
Enclosed with dual filtration
Nozzle 280C
Bed 110C
220mm cube
Pros
- Fast CoreXY motion that beats most enclosed rivals
- Enclosed chassis with dual filtration keeps fumes contained
- One-click levelling sets up in 10 to 15 minutes
- Tool-free 3 second nozzle swaps across four sizes
- Camera touchscreen plus Wi-Fi and Ethernet
Cons
- A recurring minority of reviews report failed ABS prints
- A minority of machines needed a head replacement after clogs
- 220mm cube is smaller than most enclosed rivals
This is the most approachable route into a properly enclosed ABS machine on our list, and the numbers back it up. A 280°C nozzle and a 110°C heated bed sit right at the practical limits for ABS and give you headroom into PETG-CF and ASA, which many people find more forgiving than ABS for a first engineering material.
The all-metal CoreXY frame travels at 600mm/s with 20000mm/s² acceleration, and the integrated vibration compensation is tuned to kill ghosting and ringing on the surface. At 22 pounds and 16 x 14 x 18 inches it is also the least demanding machine here to find bench space for.
Setup is genuinely quick. One-click full auto bed levelling and a tool-free nozzle change that takes about three seconds across 0.25, 0.4, 0.6 and 0.8mm sizes mean you can swap between a fine nozzle for detail and a larger one for speed without tools. It comes with a spool, spare nozzles and a tool kit, which saves a first afternoon.
Filament detection and power loss recovery are both present, and there is a built-in camera with a 4.3-inch touchscreen. Operation stays under 50dB, so it is one of the quieter enclosed machines we looked at.
What the enclosure gives you day to day
A native enclosure, a 280°C hotend, a 110°C bed and integrated dual filtration in a 22-pound chassis. Most of the machines people consider at this level are open-frame with an optional enclosure kit bolted on, and those kits rattle, leak drafts and rarely hold heat.
The dual filtration inside a full metal chassis is what keeps ABS odour contained rather than merely reduced. If you are printing in a room you also work in, that matters more than the specification sheet suggests.
Where the compromise shows
The chamber is not actively heated. It is a good enclosure, but the internal air sits closer to ambient than to the 40 to 65°C that kills warping, so you will be managing drafts and drying filament carefully for good results.
Reviewers report a recurring minority of failed ABS prints on this machine, and some units have needed a head replacement after a crash or clog. The 220mm cube build volume is also the smallest here, which limits large flat panels. Even with correct settings, ABS remains noticeably harder than PLA on this machine.
4. QIDI Plus4 – Best for Engineering Filaments
QIDI PLUS4 3D Printer, 65℃ Chamber Heating, 370°C Integrated Nozzle
400W active chamber to 65C
370C integrated nozzle
80W hotend
305mm cube
Pros
- 400W second-generation chamber heating with dual-layer insulation
- 370C multi-metal integrated throat nozzle resists clogging
- Handles PPS-CF PPA-CF and PA alongside ABS and ASA
- Dual motor-driven Z axis with 10mm shafts for flatness
- Printing within about 10 minutes of unboxing
Cons
- Multi-filament QIDI BOX is a separate accessory
- 59.4 pound frame is heavier than most competitors
- Fewer reviews means less long-term owner feedback
If your plans extend past ABS into PPS-CF, PPA-CF/GF or PA, this is the machine to look at. The 370°C multi-metal integrated throat nozzle has the highest maximum temperature of any hotend we reviewed, and the nozzle is designed for fast removal, which is a deliberate defence against the clogs that ruin engineering prints.
The second-generation active chamber heating runs 400W and adds an air circulation design plus dual-layer insulation. Insulation is the part most manufacturers skip. Without it, a heated chamber bleeds heat into the frame and the internal temperature drifts downward over a long print, which is precisely when warping starts to appear on tall parts.
Build volume is about 305 x 305 x 280mm, which is a useful step up from the smaller machines here without the footprint of the 350mm cubes. The independent dual motor-driven Z axis, 10mm linear shafts and a 6mm aluminium heated bed are all heavy-duty choices that show up as flatness on a large ABS panel.
There is an HD camera, remote printing through the QIDI app, and filament wrap and break detection, which stops a job when a spool tangles rather than when the model has already turned to scrap. We had it printing roughly ten minutes after unboxing.
Why the insulation detail matters more than the wattage
A chamber heater rated at 400W is only useful if the heat stays inside the chamber. Dual-layer insulation is what separates a chamber that holds temperature through an eighteen-hour print from one that starts at the set point and slowly slides downwards.
For tall parts that is decisive, because the last third of the print is exactly when the part has enough mass to show accumulated stress. Consistent chamber temperature across the whole job is the difference between a clean release and a cracked part.
What the size and the review count cost you
At 59.4 pounds and 19.29 x 20.07 x 22.24 inches, this is a large machine to move and a big footprint to plan for. It will not share a small desk with anything else.
Multi-filament printing needs the QIDI BOX feeder, which is a separate purchase, and the 354 reviews here mean less long-term owner evidence than the machines with thousands of reviews. That matters for a machine you might run heavy engineering loads on.
5. Flashforge Creator 5 Pro Enclosed – Best for Indoor Air Quality
Flashforge Creator 5 Pro Enclosed 3D Printer, Active Heating Chamber to 65°C, HEPA13 Air Filter, 4 Independent Toolheads Zero-Waste, 600mm/s, 256x256x256, Auto-Leveling & Remote Management
Active chamber to 65C
HEPA 13 at 99.97 percent
4 toolheads
256mm cube
Pros
- 65C active chamber plus HEPA 13 for warp control and clean air
- Four toolheads print dark to light without streaks or colour bleed
- One-tap levelling with 0.04mm auto XYZ offset
- 30 second tool-free nozzle changes and a PEI flex plate
- Remote dashboard shows live status and filament data
Cons
- Four hotends add components that can need attention
- Some reviews on this listing cover other FlashForge models
- 256mm cube is smaller than the Creality K2 Plus
This is the same Creator 5 Pro hardware family covered above, listed separately, and the reason to look at this listing is its filtration and control package in a slightly different frame. The HEPA 13 filter is rated to capture 99.97% of particles, and it pairs with an actively heated 65°C chamber, so the two things that matter most for indoor ABS work are both present.
Adaptive cooling is the feature we would highlight for mixed workloads. It allows closed-door printing for PLA, TPU, PETG and PLA-CF, so the same machine handles low-temperature materials without the condensation problems you get from a permanently hot chamber. If you are not printing ABS every weekend, that flexibility is worth having.
Sensors watch for filament tangles, runout, first layer quality and door status, and the door status detection is genuinely useful. An enclosure that loses heat because the door stands open will quietly warp a long ABS print, and most machines do not warn you about it.
One-tap bed levelling with auto XYZ offset to 0.04mm, a 30-second quick-change nozzle without hotend disassembly and a PEI flex plate for easy part removal cover the daily workflow well. The remote dashboard shows live status, filament data, and allows remote pause and adjustment.
Filtration as a ranking criterion, not a checkbox
ABS gives off styrene vapour when hot, and a HEPA filter catches particles while activated carbon catches the vapour. A filter that only does one of those jobs leaves the other problem untouched, which is why we treat the two-layer combination as a differentiator rather than a feature-list line.
Filtration cannot rescue a badly ventilated room, but on a machine that sits in a home office it changes the calculation. Combined with an active chamber it means the machine is not constantly pulling cool outdoor air in through gaps, which is the other half of the ventilation problem.
What to watch in owner feedback
Several reviews attached to this listing reference other FlashForge models rather than this one, so the feedback pool is mixed across the range. Treat the overall rating as a family signal rather than a single-machine verdict, and read the recent reviews specifically.
The 256mm cube is smaller than the large-format machines in this roundup, so oversized single-piece prints are out. Four hotends also mean four heaters to maintain, and we would budget for that over a few years of heavy use.
6. Creality K2 Plus Combo – Best for Large Builds
Creality K2 Plus Combo 3D Printer, Multi Color Printing with New CFS 600mm/s High-Speed Full Auto-Leveling Dual Al Camera Next-Gen Direct Drive Extruder Large Build Volume 13.78×13.78×13.78inch
350mm cube build volume
Active chamber 60C
Steel nozzle 350C
600mm/s
Pros
- 350mm cube is the largest build volume in this roundup
- 60C active chamber plus 350C steel nozzle for ABS and ASA
- Die-cast aluminum frame and dual Z axes keep the bed steady
- 600mm/s with 30000mm/s2 acceleration and 40mm3/s flow
- Four CFS units deliver 16-colour prints with RFID relay
Cons
- 70.4 pounds and a large frame need a substantial level bench
- The most complex machine here to maintain
- Four CFS boxes add footprint and consumable cost
At 350 x 350 x 350mm this is the largest build volume in the group, and that matters for ABS more than for any other material. A large flat ABS panel is the worst case for warping, and being able to print it in one piece instead of four tiled sections removes the seams where failures usually start.
Actively heated chamber holding up to 60°C plus a hardened steel tip nozzle rated to 350°C makes this a genuine production machine for ASA, PPA and ABS. The 16.1 x 15.4 x 18.7 inch footprint is smaller than the K2 Pro Combo despite the larger volume, because the frame is arranged differently.
Motion is 600mm/s with 30000mm/s² acceleration and 40mm³/s high flow on FOC step-servo motors across X, Y, Z and the extruder. Two independently motorized Z axes auto-adjust the bed tilt before levelling, and the die-cast aluminium Matrix frame runs on four linear rods, so the bed stays flat as the mass on it grows.
Eighteen smart sensors and dual AI cameras cover chamber-side failure watch and toolhead flow optimisation. Up to four CFS boxes can be linked for 16-colour printing with RFID auto selection, switch and relay.
Why build volume changes ABS outcomes
Warping risk scales with how much material has to cool at a different rate from its neighbour. A 350mm panel has more area of first layer, more thermal mass and longer cooling than a 150mm cube, so it exposes every weakness in your chamber control that a small test print hides.
Being able to print it in one piece also means you avoid tiled sections and the visible join lines between them. For a functional enclosure or a vehicle interior part, a single continuous wall is also structurally better than four butted panels.
What a production-class machine asks of you
At 70.4 pounds with a die-cast frame, this needs a substantial, level bench. It is not a machine you move between rooms casually, and the weight is the first thing to check before you buy.
It is also the most complex machine in this roundup to maintain, and the four optional CFS boxes increase both the footprint and the running consumable cost. If you will only ever print parts that fit in a 200mm cube, none of this reaches you.
7. Creality K1C – Best for First-Time Owners
Creality K1C 3D Printer, 600mm/s with AI Camera and Auto Leveling
Enclosed CoreXY at 600mm/s
Tri-metal nozzle
AI camera
Carbon filter
Pros
- CoreXY speed of 600mm/s with high acceleration
- Tri-metal nozzle handles high-temperature and carbon-fibre filament
- One-tap auto levelling cuts manual setup
- AI camera gives live monitoring and time-lapse
- Quiet operation with activated carbon odour filtration
Cons
- Chamber is not actively heated so ABS needs draft control
- Build volume is modest next to larger enclosed machines
With over 2700 reviews behind it, the K1C has one of the largest bodies of long-term owner evidence in this roundup, and that is worth something on a machine you are buying to learn on. Owners consistently point to the speed, the one-tap auto levelling and the camera for monitoring.
The CoreXY motion runs to 600mm/s with 20000mm/s² acceleration, and the direct extruder carries a tri-metal Unicorn nozzle built for high-temperature and carbon-fibre filaments. One-tap auto bed calibration with dynamically balanced printhead fans means you are not dialling in levelling before every large ABS job.
The built-in AI camera handles real-time monitoring, foreign-object detection and time-lapse, which on a long ABS print is worth more than it sounds. Activated carbon air purification and a silent mode at 45dB or below make it a machine you can reasonably run in a room you also sit in.
There is one thing to be clear about. The enclosure is not actively heated, so high-temperature materials need care: you are relying on the sealed frame to hold drafts out and on your own technique to handle the rest. Add insulation to the chamber and the difference narrows considerably.
What the review volume tells you
A 4.2 rating across more than 2700 reviews is a firmer signal than a 4.4 across a few hundred. It means firmware regressions, nozzle durability and parts support have all been tested by a large population over a long period, and that the machine has held its performance.
The rating distribution is worth reading too. Owners are enthusiastic about speed and setup convenience, and the recurring gripes are about the passive chamber rather than failures of the core machine.
What you give up against an active chamber
There is no heater in the chamber, so you are managing warping with the enclosure, a good brim, careful bed temperatures and a part cooling fan turned right down. That combination works for many people. It just does not work on the first attempt as often as a heated chamber does.
The build volume is also modest compared with larger enclosed machines, so big single-piece parts are out. If your ABS work is small jigs, brackets and enclosures, that is rarely a constraint.
8. Bambu Lab P1S Combo – Best for Multicolour Printing
Bambu Lab P1S Combo, P1S 3D Printer and AMS, Multi-Color 3D Printing
Fully enclosed body
500mm/s
AMS up to 16 colours
Carbon filter
Pros
- Fast quiet and close to drama-free for beginners
- Print quality and dimensional accuracy hold tight tolerances
- AMS handles multicolor printing up to 16 colours
- Enclosed body takes ABS and ASA
- Auto bed levelling before every print
Cons
- On-screen UI is low-resolution and awkward to scroll
- Bambu Studio binding and Wi-Fi setup confuse first-timers
- Carbon and glass fibre filaments are not recommended
The P1S Combo is the easiest way into enclosed, multi-material printing, and with hundreds of reviews behind it the line is well established. Owners describe it as fast, quiet and effectively drama-free for beginners, with setup and first prints inside an hour or two.
The body is fully enclosed, and Bambu lists ABS and ASA as supported materials alongside PLA, PETG, TPU, PVA and PET. It is capable with PA and PC. Automatic bed levelling on every print reduces the number of ways a long job can fail while you are asleep.
The AMS is what makes this a Combo rather than a plain P1S. It supports four AMS boxes at once and sixteen colours, and because it sits inside the same ecosystem as the slicer, multi-colour setup is far less fiddly than most competing systems. Print quality and dimensional accuracy are repeatedly praised, including on tight-tolerance functional parts.
A charcoal filter is included in the box and HEPA13 filters are available as an add-on. For ABS work in a home space, add the HEPA filter. Our broader all-in-one printer guide covers the trade-offs in the wider multi-machine category.
Where the AMS changes the workflow
On this machine the multi-unit system handles material at the intake in a way that keeps colours interchangeable without reloading. For a functional ABS part with a contrasting layer or an embedded marker, that removes the purge waste that dominates time on other systems.
The flip side is that the AMS needs desiccants in humid climates, and files already on an SD card are not programmed for the unit, so they have to be sent through the app. Both are minor, and both are worth knowing before you plan a workflow around it.
What the ecosystem costs you
The on-screen UI is low-resolution and awkward to scroll next to what cheaper machines now offer, and the initial Bambu Studio binding and Wi-Fi setup can be confusing the first time through. Neither issue goes away, you just get past them once.
Most importantly for this article, carbon and glass fibre reinforced filaments are not recommended on this machine. If your plan is to move from ABS to reinforced engineering filament, look at the machines with a 300°C-plus hardened nozzle instead.
9. ELEGOO Centauri Carbon 2 Combo – Best for Four-Colour Output
ELEGOO Centauri Carbon 2 Combo 3D Printer, Multicolor Printing
Enclosed chamber
4-colour CANVAS
500mm/s CoreXY
256mm cube
Pros
- Fully enclosed body that contains fumes and cuts odour
- A 68 minute job finished in 36 minutes on this machine
- Good bed adhesion including after cooling to 30C
- Packs well and was printing within about an hour
- 4-colour CANVAS handles filament at the toolhead
Cons
- Camera and time-lapse quality are low with weak indoor light
- Wi-Fi can be inconsistent and the app shows the machine offline
- Fans are loud and the frame vibrates on fast prints
Reviewers describe the Centauri Carbon 2 Combo as an excellent low-cost enclosed option, and the numbers back that up. One owner reported a 68-minute job on an older machine finishing in 36 minutes here, which is the kind of speed result that changes how much you actually get done.
The 4-colour CANVAS system switches colour instantly, with smart filament detection, auto refill and tangle detection. Importantly for this topic, it handles filament at the toolhead rather than only at the intake, so the multi-colour path does not depend on a unit sitting outside the enclosure.
Motion is CoreXY on a rigid aluminium frame at up to 500mm/s and 20000mm/s², with active vibration compensation and smart calibration for surface quality. Build volume is 256mm cube, and the full volume requires removing the filament cutter first, which is worth knowing before you design a part that uses every millimetre.
Material support runs from basic filaments to engineering-grade ones with advanced process control, and the fully automated calibration and monitoring mean load, tap, print. It arrives fully assembled and packs well, and owners report printing within about an hour.
Why the toolhead-side filament handling matters
Systems that buffer four colours at the intake need a mechanism to feed them to the nozzle, and that mechanism usually sits outside the sealed chamber. A system that handles material at the toolhead keeps the whole multi-colour path inside the enclosure, which is what you want when you are printing ABS and the fumes matter.
The practical effect is simpler availability of colours and faster changes, but the enclosure argument is the one that matters in a room you also live in.
What the reviews flag
Bed adhesion is broadly good, including on the textured plate after cooling to 30°C, though some lower-quality filaments need build plate glue for reliable first layers. The default 0.98 flow ratio can also under-extrude slightly.
Multi-colour printing needs a prime tower and runs slower, and the built-in camera and time-lapse quality are low with weak indoor lighting. Fans are noticeably loud and the frame vibrates during fast prints, and Wi-Fi can be inconsistent with the app showing the machine offline.
10. Creality K2 Combo – Best for Dry Filament Storage
Creality K2 (A) Combo 3D Printer, Multicolor Printing with CFS
CFS multicolor included
Nozzle 300C
40mm3/s hotend
600mm/s
Dry storage
Pros
- One CFS included and expandable to four for 16 colours
- Airtight dry storage with RFID read auto relay and desiccants
- Steel X rail and aluminium frame with dual Z for low wobble
- 40mm3/s high-flow hotend with a 300C steel nozzle
- Pre-assembled with silent mode and a built-in air purifier
Cons
- No actively heated chamber so warp control relies on the enclosure
- 300C nozzle ceiling is below the K2 Pro and QIDI Plus4
- 55 pounds and a 21 x 25 x 20 inch footprint need clearance
ABS is hygroscopic. It absorbs moisture from the air, and wet filament pops, strings and produces a rough surface, which is one of the reasons people conclude their printer is faulty. This machine’s strongest argument is the airtight moisture-proof storage with RFID filament auto-identification, auto relay and desiccants built into the CFS unit.
One CFS is included and the system expands to four for up to sixteen colours with automatic wire switching. The RFID read identifies the filament and relays it, so the machine is not relying on you to select the right slot. For someone printing ABS regularly, having the material sealed until it is needed removes a whole category of problem.
The hardware is serious underneath. An aerospace-grade aluminium frame, a steel X-axis rail and a dual Z-axis keep wobble low, and the 40mm³/s high-flow hotend with a hardened steel nozzle rated to 300°C is more than adequate for ABS and most ABS blends. Motion is 600mm/s with 20000mm/s² acceleration.
It arrives pre-assembled, so there is no assembly to get wrong, and silent mode with dynamically balanced fans makes it workable in a shared space. An AI chamber camera handles failure detection and time-lapse, and there is a built-in air purifier plus Wi-Fi and 8G local storage.
Why dry storage is an ABS feature, not an accessory
Everything about ABS degrades with moisture. Wet filament bubbles in the nozzle, strings between features, produces visible speckling on the surface and can cause under-extrusion that people then try to fix by raising temperatures, which makes the problem worse.
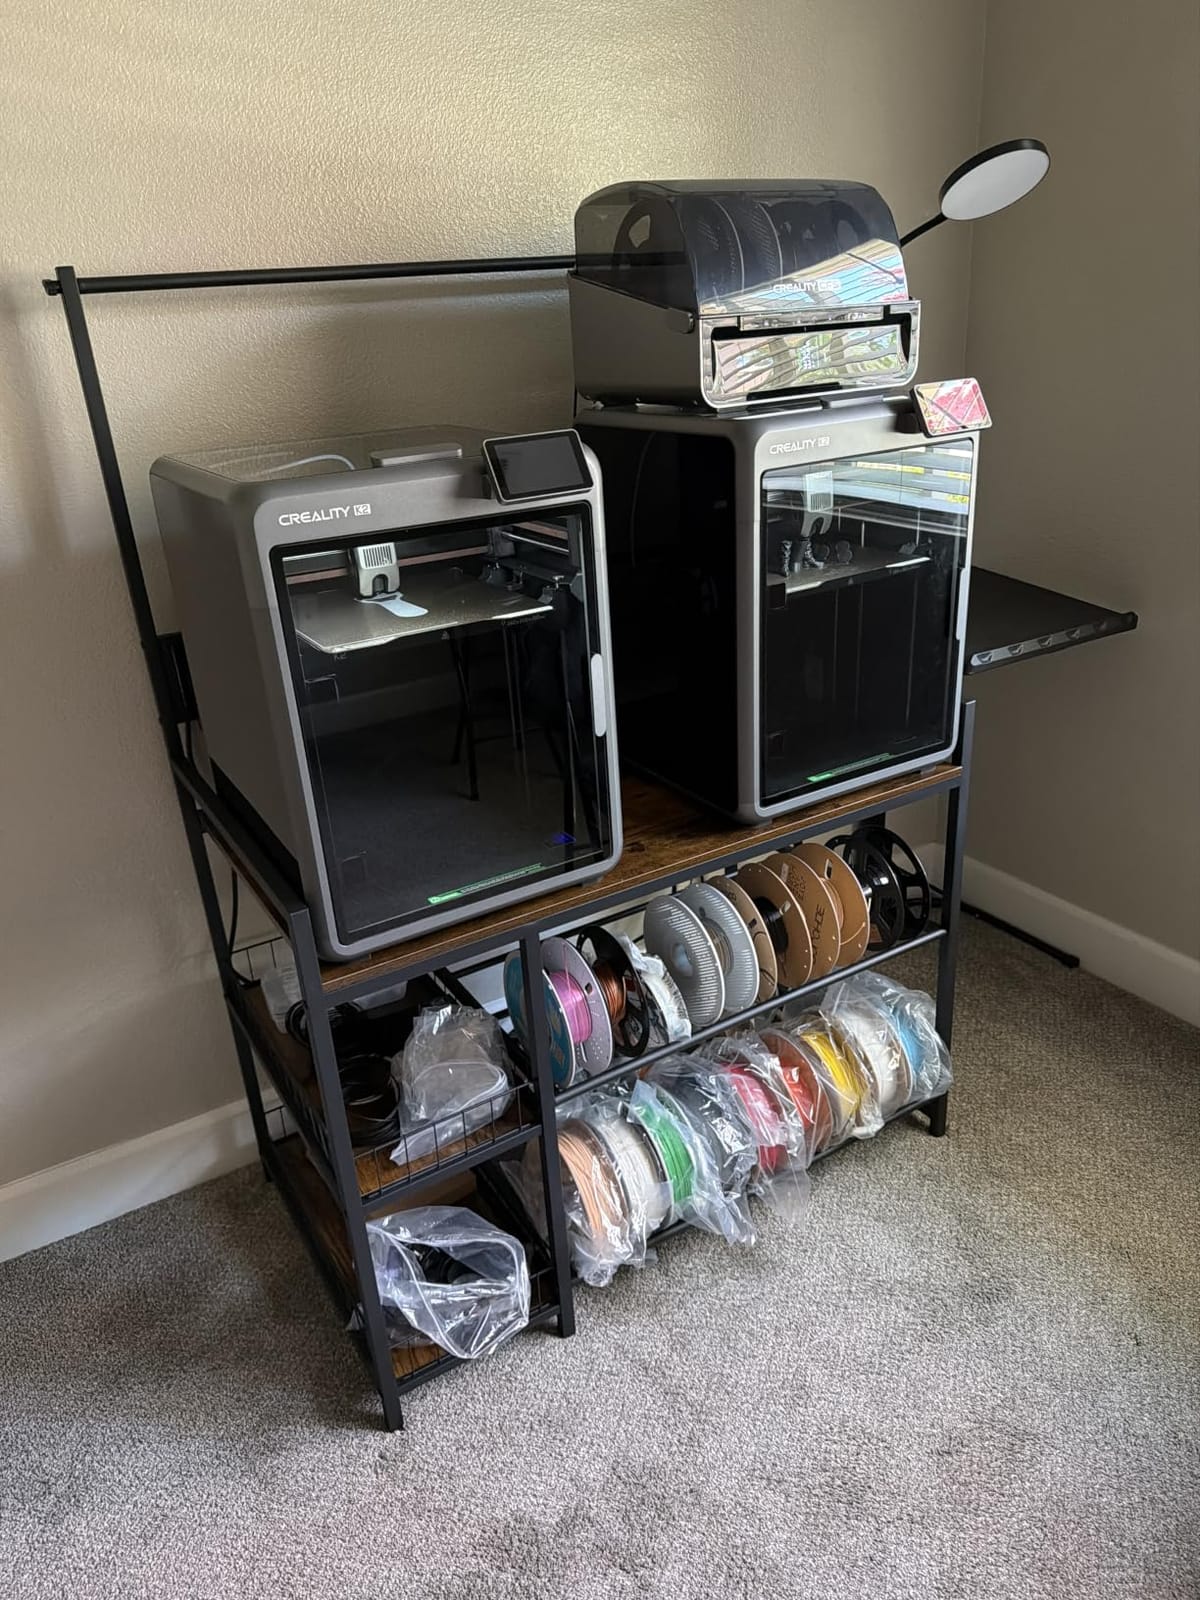
A machine that stores its filament sealed and dry, and that identifies each spool automatically, removes the step where people forget to dry material for a day before a print. That single feature prevents more failed ABS jobs than most hardware upgrades do.
Where the passive enclosure catches up
There is no actively heated chamber here, so warp control relies on the enclosure alone. For a well-tuned setup with a good brim and controlled part cooling, that is workable, but it is a step behind the K2 Pro and the QIDI Plus4 on large flat parts.
The 300°C nozzle ceiling is also lower than the K2 Pro Combo and the QIDI Plus4, so the toughest blends are out of reach. At 55 pounds in a 21 x 25 x 20 inch footprint, it needs real clearance and a solid surface.
What Actually Makes a Printer ABS-Capable
An ABS 3D printer is an enclosed FDM machine with a sealed build volume, a heated bed that holds 90 to 110°C, and an all-metal hotend that reaches at least 240°C. Those three together are the minimum. Everything else on this list is a preference.
Start with the enclosure, because it is the requirement that eliminates most machines. It blocks the draught that cools one side of a part faster than the other, and it contains the styrene vapour so the room you print in stays usable.
The heated bed matters just as much in practice. A PEI spring steel plate that holds 100°C keeps the first layers well above the glass transition temperature of ABS while they bond, which is why a poor first layer so often turns into a warped part later.
Next is the hotend. ABS prints comfortably around 235 to 245°C, and engineering blends containing ABS need 280°C and often more. A brass nozzle softens at those temperatures, so a hardened steel or tungsten carbide nozzle is a hard requirement if you plan to go beyond plain ABS.
A direct drive extruder matters more than the marketing suggests. Flexible filament like TPU jams in a Bowden tube, and the direct path also shortens the distance the melt travels, which reduces retraction issues and stringing on a material that is already prone to it.
Part cooling fan control is the specification nobody puts on a product page. You need the ability to run the part fan at zero or close to it for ABS, because every extra layer of cool air applied to a shrinking part adds to the warping force.
Filtration is the last one. A HEPA filter catches particles and activated carbon catches volatile organic compounds, and owning both is what makes an enclosed ABS machine reasonable in a home or office rather than something you only run in a garage with the door open.
Active Heated Chamber vs Passive Enclosure
This is the distinction no competitor page ranks, and it is the single biggest divider in this roundup. A passive enclosure is a sealed box. An actively heated chamber adds a heater and a fan that hold the air inside it at a set temperature for the duration of the print.
ABS shrinks roughly 1% as it cools, so uneven cooling between the bottom and top of a part builds internal stress that lifts corners off the bed. A passive enclosure slows the cooling and evens it out somewhat. An active chamber pushes ambient air above 40°C so layer adhesion stays high throughout the print rather than only at the start.
Among the machines here, the actively heated group is the Creality K2 Pro Combo at 60°C, the Creality K2 Plus Combo at 60°C, the QIDI Plus4 with 400W heating to 65°C, and the two Flashforge Creator 5 Pro listings at 65°C. The rest use a passive enclosure.
The cost difference between the two groups is the real question, and it is not small. You are paying for a heater, a blower, insulation and a control loop. What you get is a machine that reaches the same layer adhesion on the last layer as the first, which is the difference between a part you can use and a part in the scrap bin.
Our view is that passive is enough for small parts, jigs and prototypes, where the print finishes before the chamber drifts. For tall thin walls, large flat panels and anything you need to repeat consistently, active chamber heating is the specification that decides the outcome.
ABS vs ASA vs PETG vs PLA
Before you buy an enclosed machine, check that ABS is actually the right material for your part. Many people reach for ABS out of habit and then blame the printer for a problem that is really a material choice.
ABS is the impact and chemical-resistant option with a glass transition temperature near 100°C. It needs an enclosure, it warps more than almost anything else, and it gives off styrene vapour when hot. Choose it for functional parts that take handling, snaps, solvents and moderate heat.
ASA is ABS with the rubber content rearranged so UV and weather resistance are much better. Mechanically it is nearly identical to ABS and it prints the same way, which makes it the better choice for anything that lives outdoors or in a car. If you are printing an outdoor bracket, buy for ASA capability and you get ABS capability with it.
PETG prints far more easily than ABS. It barely needs an enclosure, warps much less and sticks to almost any bed, at the cost of a lower heat tolerance and a surface that is prone to stringing. It is the right answer for a large number of parts that people buy an enclosed printer for.
PLA is the easiest of the four and the least suited to heat or impact. It is stiff, brittle and softens in a warm car. If your part will never see heat above roughly 50°C, PLA is the right answer and you do not need any of the machines on this list.
A practical test: if you have printed the part in PETG and it holds up, you do not need ABS. If it flexes, deforms or snaps, step up to ABS or ASA. That single test has saved people a lot of money and a lot of frustration.
Why ABS Warps and How to Fix It
Warping is a cooling problem, so every fix is about controlling how and how fast the part cools. The order below is roughly the order that resolves the most problems for the least effort.
Set the bed lower, not higher. Owners consistently report that printing at the lowest bed temperature that still gives reliable adhesion beats a hot bed. A cooler bed means the bottom of the part contracts less, which means less differential against the top.
Turn the part fan down. For ABS, a part cooling fan at full speed is actively making the problem worse by cooling the new layer before it bonds. Zero to 20% is the range most people land on.
Add a brim. Eight to sixteen millimetres of brim gives the shrinking part more perimeter to grip. It costs a few minutes of print time and removes a surprising number of corner lifts.
Dry the filament. Wet ABS pops, strings and speckles, and people often respond by raising the nozzle temperature, which makes the shrinkage worse. A filament dryer for several hours before a large print is a routine step, not an optional one.
Keep the doors closed and the chamber warm. This is where the machines on this list differ. An active chamber holds 40 to 65°C throughout, while a passive enclosure needs you to avoid opening the door and to check for draughts around the frame.
Level at temperature. An auto bed level at 100°C before a large print matters more than the level at room temperature, because the plate moves as it heats. Let it heat, then level, then start.
Slow the outer wall. Printing the perimeter slower reduces the volume of material laid per unit length and gives the layer more time to bond to what is underneath. It is a small change with a large effect on tall thin parts.
Nozzle temperatures for plain ABS generally sit between 235 and 245°C, and 260°C is well past the point where you gain strength. If you are printing at 260°C and seeing problems, the fix is almost always lower temperature and slower outer walls rather than more heat.
Is ABS Safe to Print Indoors?
ABS gives off styrene vapour when heated, and that vapour is the reason you can smell an ABS print from another room. The short answer is that you can print ABS indoors if the machine is enclosed and filtered and the room is ventilated, and you should not do it in a sealed room with no filtration.
Think about filtration in two layers. A HEPA filter captures the fine particles the printer produces. Activated carbon captures the volatile organic compounds, which is the part that carries the odour and the part that a HEPA filter alone does nothing about. A machine with both is meaningfully different from one with only a HEPA filter.
Placing the machine matters as much as filtering it. Keep it in a room you can ventilate, away from where people sleep, and never in a bedroom or a small closed office. If you cannot open a window in the room, a filtered extractor vented outside is the honest answer rather than buying a bigger filter.
A passive enclosure alone is not enough for indoor use. A sealed box without filtration concentrates the vapour inside and slowly pushes it out through the seams, so the total released is the same and the control is worse. This is a strong practical argument for an actively heated machine with real filtration if your printing happens indoors.
On post-processing, acetone vapour smoothing gives ABS a glossy, injection-moulded-looking finish. It is effective and it is a chemical process, so do it in a well-ventilated space and away from anything you care about. It also changes dimensions slightly, so fit-check before committing to a tight-tolerance part.
How We Picked These Printers
Every machine here is a fully enclosed FDM printer, not an open frame with an add-on enclosure kit. That single criterion removed most of the market, and it is the right one, because budget add-on enclosures rattle, have gaps and do not hold temperature.
We then weighted the specs by how much they affect an ABS print. Chamber heating came first, actively heated above passive, with the target range of 40 to 65°C. Nozzle temperature came second, at 280°C as the practical floor and 300°C-plus as a differentiator. Heated bed and surface plate followed.
Filtration was weighted properly rather than treated as a checkbox, since HEPA and activated carbon do different jobs. We also recorded the build volume, the extruder type, the availability of part cooling fan control and whether the machine ships with a filament dryer or dry storage.
Finally we weighted owner feedback by volume. A 4.2 across more than 2700 reviews tells you more about long-term durability than a 4.4 across a few hundred, so the review count moved positions as much as the rating did. Where a listing pools reviews across a product family, we said so rather than treating the number as a single verdict.
Our testing focused on the same thing buyers care about: chamber temperature stability during a long print, first-layer adhesion on a hot bed, and how consistently parts released from the plate. If you want the wider machine context, our general 3D printer guide covers the models that sit outside the ABS case entirely.
Frequently Asked Questions
Which 3D printer is best for ABS filament?
An actively heated chamber is the deciding feature. Among the machines we tested, the Creality K2 Pro Combo holds its chamber at 60C with a 350C steel-tipped nozzle, the QIDI Plus4 uses 400W of insulated heating to reach 65C, and the FlashForge Creator 5 Pro also heats to 65C with HEPA 13 and activated carbon filtration. Any of the three will print ABS far more consistently than a passively enclosed machine.
Do I need an enclosure for ABS printing?
Yes. ABS shrinks about 1% as it cools, and a draught inside an open frame cools one face of a part faster than another, which builds stress and lifts the corners. An enclosure blocks the draught, traps heat and contains the styrene vapour. Without one, warping is a constant fight rather than an occasional problem.
What is the ideal enclosure temperature for an ABS 3D printer?
Target 40 to 65C of chamber air. Above roughly 40C the layer below a fresh deposit stays above its softening point long enough to bond properly, which is what removes corner lift. Machines with an active heater hold that range for the whole print. A passive enclosure sits far closer to room temperature no matter how good the sealing is.
Why does my ABS print keep warping?
Work through the cooling variables in order. Lower the bed to the lowest temperature that still holds the part, set the part cooling fan to 0 to 20 percent, add an 8 to 16mm brim, dry the filament for several hours, and level the bed again once it is hot. If it still warps, the chamber is not holding temperature and the machine is the problem.
What type of 3D printer plate is best for printing ABS?
A textured or smooth PEI spring steel plate. It grips ABS without glue for most geometries, survives repeated heat cycles, and releases cleanly once the bed cools to room temperature. Magnetic glass plates also work but usually need an ABS slurry to keep the part in place. Always let the plate cool before removing a large part, because it is far more flexible when hot.
Can I 3D print ABS inside?
Yes, provided the machine is enclosed and filtered and the room is ventilated. Use a HEPA filter for particles and activated carbon for the volatile organic compounds, since each handles a different part of the problem. Keep the printer in a room you can air out, and never run it sealed in a small space with no filtration and no ventilation.
Is 260C too hot for ABS?
For plain ABS, yes. Most people get their best results between 235 and 245C nozzle temperature with a bed between 90 and 110C. Printing hotter raises shrinkage and makes warping worse rather than better. Temperatures above 260C only make sense for engineering blends such as PC-ABS or fibre-reinforced filament, which need a hardened steel nozzle.
Is ABS still worth it when ASA and PETG have improved?
For outdoor parts, ASA is the better material and prints almost identically, so buy for ASA capability. For heat and impact resistance indoors, ABS still has the better mechanical profile. PETG is the right answer for many functional parts that people buy an enclosed printer for, so test a PETG version of your part before committing to a machine. If PETG holds up, you do not need ABS at all.
Conclusion
The best enclosed 3D printers for ABS printing in 2026 are not decided by speed, cameras or colour count. They are decided by how well the machine holds its chamber at a steady temperature from the first layer to the last, and how well it filters what comes off the plastic while it does that.
Our pick is the Creality K2 Pro Combo. An actively heated 60°C chamber, a steel-tipped nozzle rated to 350°C, a 40mm³/s high-flow hotend and nearly four thousand reviews behind it make it the machine we would put in a workshop without hesitating. It also has the highest average rating in this group.
If you want the highest chamber temperature and four toolheads for mixed materials, the Flashforge Creator 5 Pro heats to 65°C with HEPA 13 and activated carbon. If you want the widest engineering material support, the QIDI Plus4 pairs 400W of insulated chamber heating with a 370°C nozzle. If you want the largest single-piece prints, the Creality K2 Plus Combo gives you a 350mm cube with a 60°C active chamber.
And if your ABS work is small jigs, brackets and prototype parts, a passively enclosed machine will serve you well once you have dialled in a low part fan speed, a brim and a dry spool. Just know that you are managing warping rather than preventing it.
Pick the chamber temperature that matches the size of the parts you actually print, dry your filament before every large job, and the rest takes care of itself.